Leading Conveyor Manufacturer in New York, NY
Optimize your production line with tailored solutions from Excellent Conveyor—the industry-trusted conveyor manufacturer in New York, NY. We specialize in innovative conveyor system engineering, crafting custom stainless-steel sanitary conveyor systems and versatile material-handling conveyors that empower industries—from bakery to beverage, dairy to recycling—to enhance efficiency, safety, and sanitation.
With our innovative solutions, your operations will run smoother, faster, and smarter, driving your business forward with confidence.
End-to-End Solutions—From Design to Installation
Our comprehensive services encompass expert application engineering, full in-house design and manufacturing, plus seamless equipment and controls integration. By offering custom configurations, precise dimensions, and specialized components, we craft conveyor solutions perfectly aligned with your unique material handling requirements. Our core capabilities include:
- Stainless-Steel Conveyor Manufacturing
- Material-Handling Systems Maintenance
- Food Processing Automation
- Repairs and Emergency Services
- Spare Parts Supply
Excellence in Quality Manufacturing
We deliver stainless-steel sanitary conveyors alongside critical machinery, such as casers, stackers, and accumulation tables, ideally suited for food, dairy, beverage, and other large-scale production environments. To support your operations in the long term, we maintain an extensive inventory of conveyor parts and accessories, with in-stock items available for shipment within 24 hours.
Additionally, our expertise spans customized metalwork and non-sanitary solutions—ranging from luggage and pallet roller conveyors to stainless-steel and aluminum shelving, food-processing tables, covers, steps, framing, and store fixtures tailored for the restaurant, retail, and service industries. Simply put, if it’s fabricated from steel or aluminum, we can make it for you.
Streamlined Installation for Maximum Convenience
Every conveyor and piece of equipment undergoes meticulous assembly, testing, and “match-marking,” then is custom-crated before shipment. This thorough preparation makes on-site installation straightforward and efficient. From the initial filler machine to the final palletizing, we provide turnkey solutions that cover your entire technological process.
Customized Engineering Expertise
Our seasoned engineering team delivers custom conveyor and material-handling system designs, including specialty equipment engineered to the most exacting specifications. Utilizing detailed drawings and technical specifications ensures we manufacture conveyors that precisely meet your operational challenges.
We also offer a wide selection of pre-engineered conveyor solutions trusted by the food, beverage, pharmaceutical, and mass-production industries. Having crafted thousands of conveyors for a diverse client base, we’re ready to deliver an optimal fit for your project.
Plant and Equipment Surveying Services
If your facility lacks comprehensive computerized layouts, elevations, or equipment plans, we offer precise measurement services. We deliver detailed AutoCAD and PDF drawings based on thorough on-site surveys, billed on an hourly basis.
Our Specialty
Sanitary Conveyors
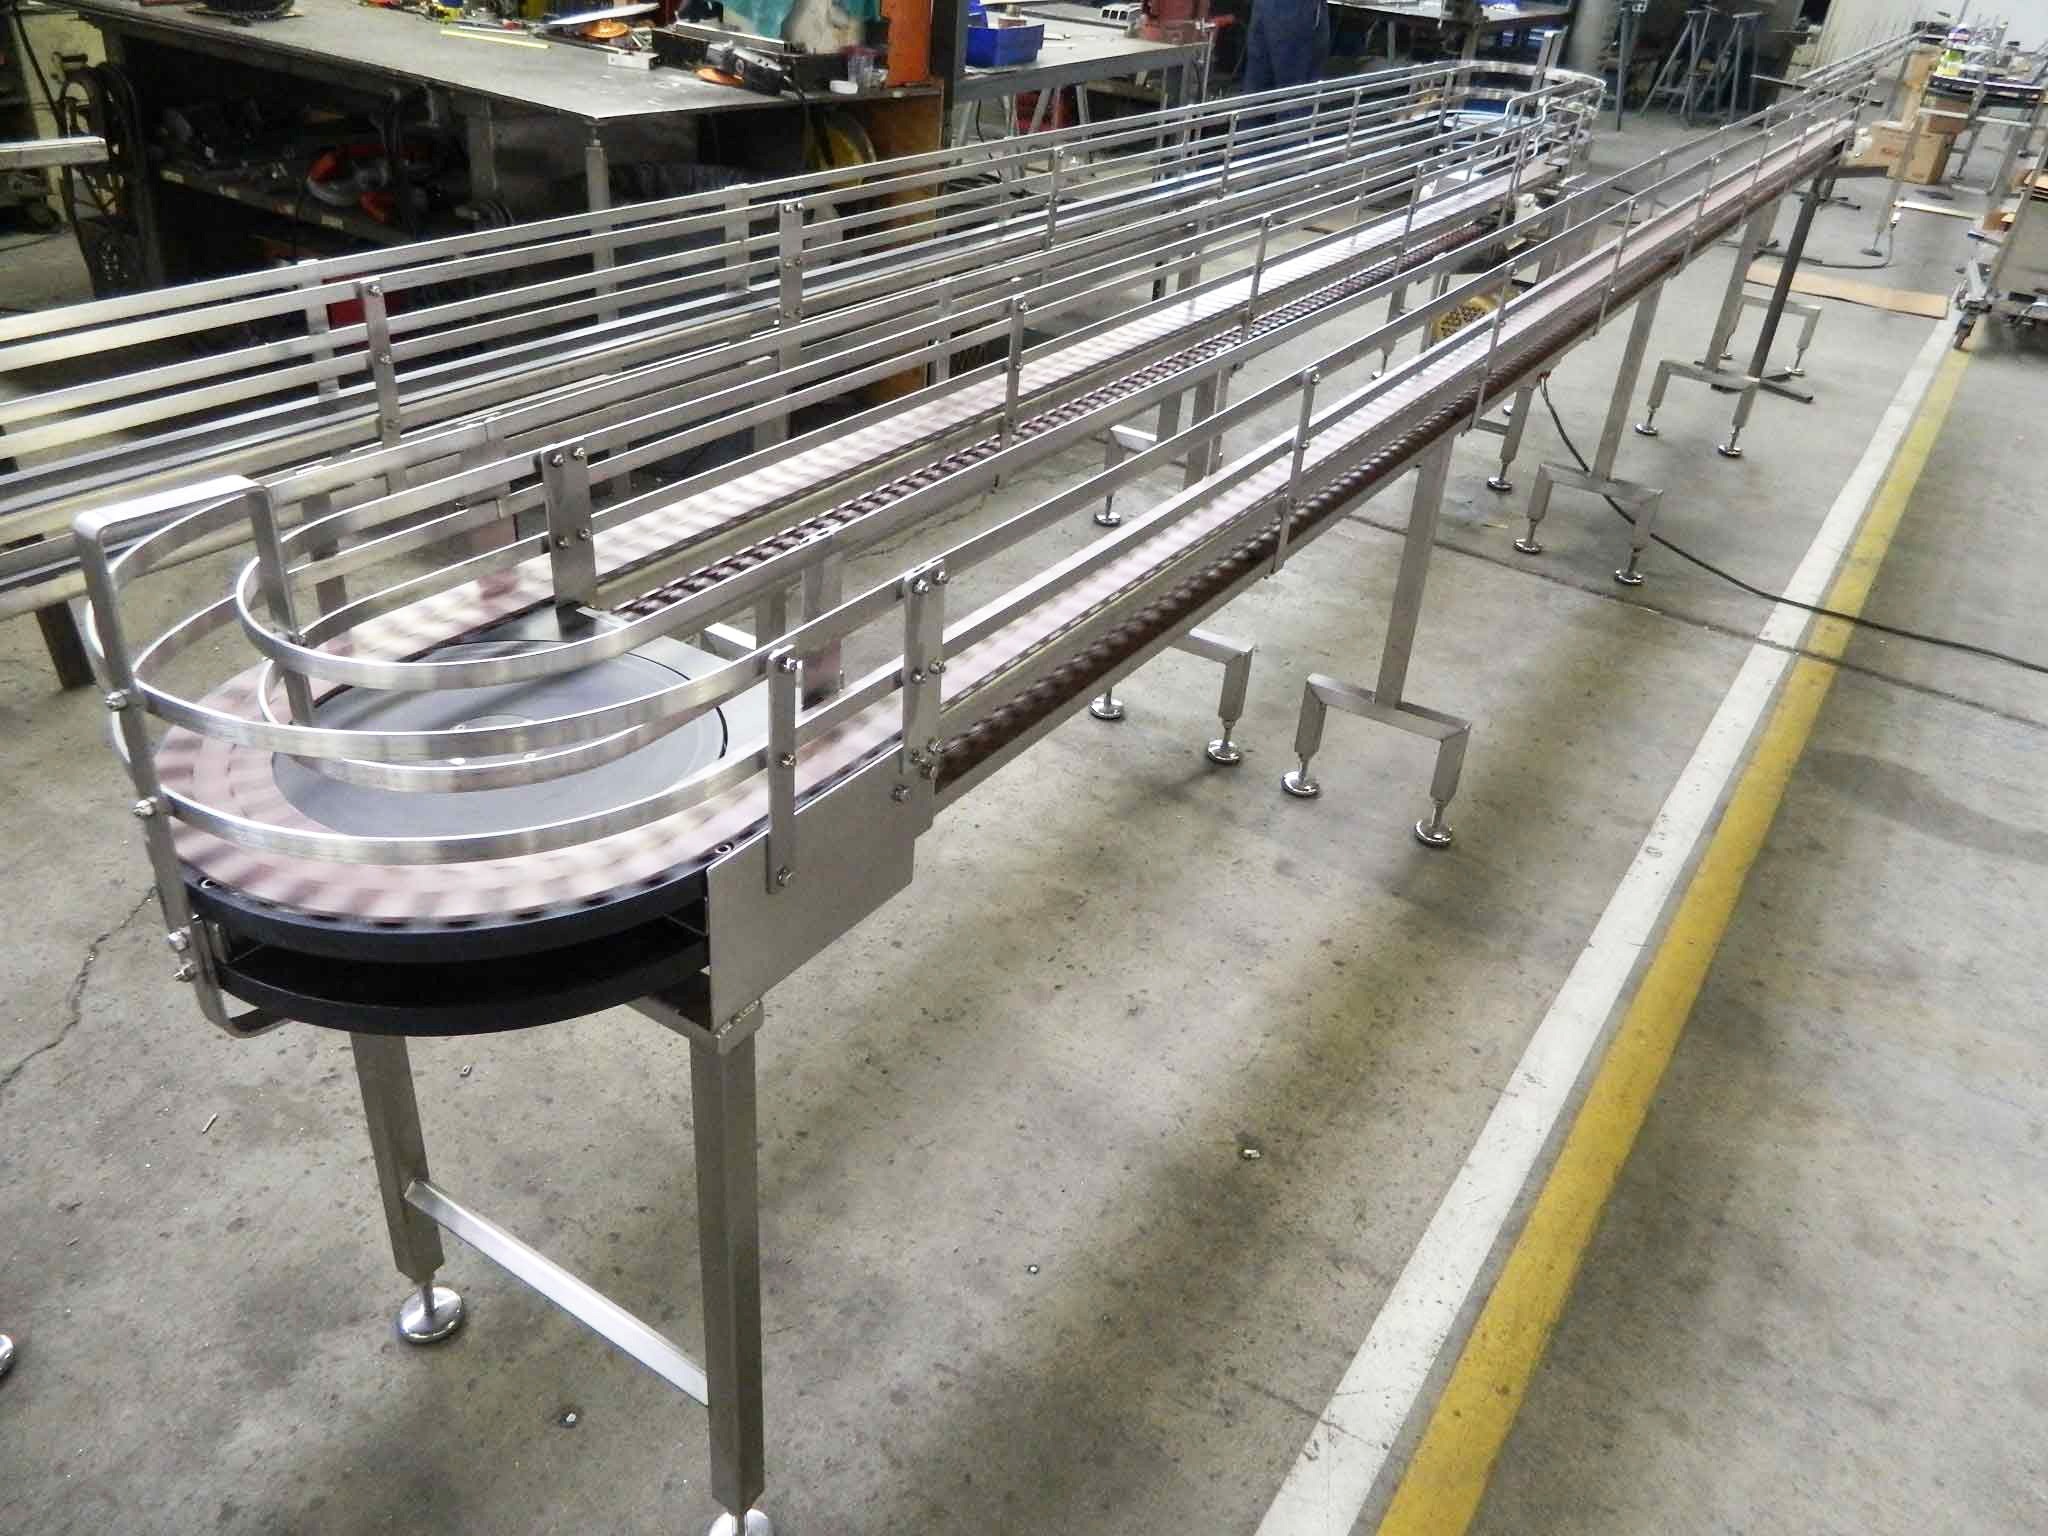
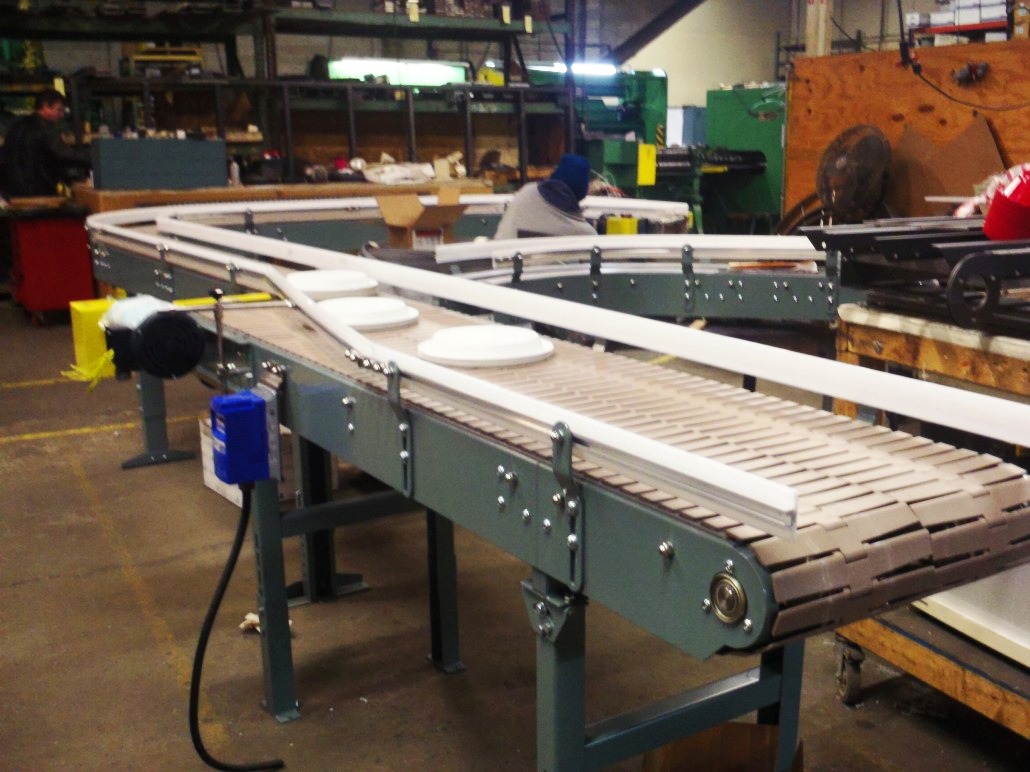
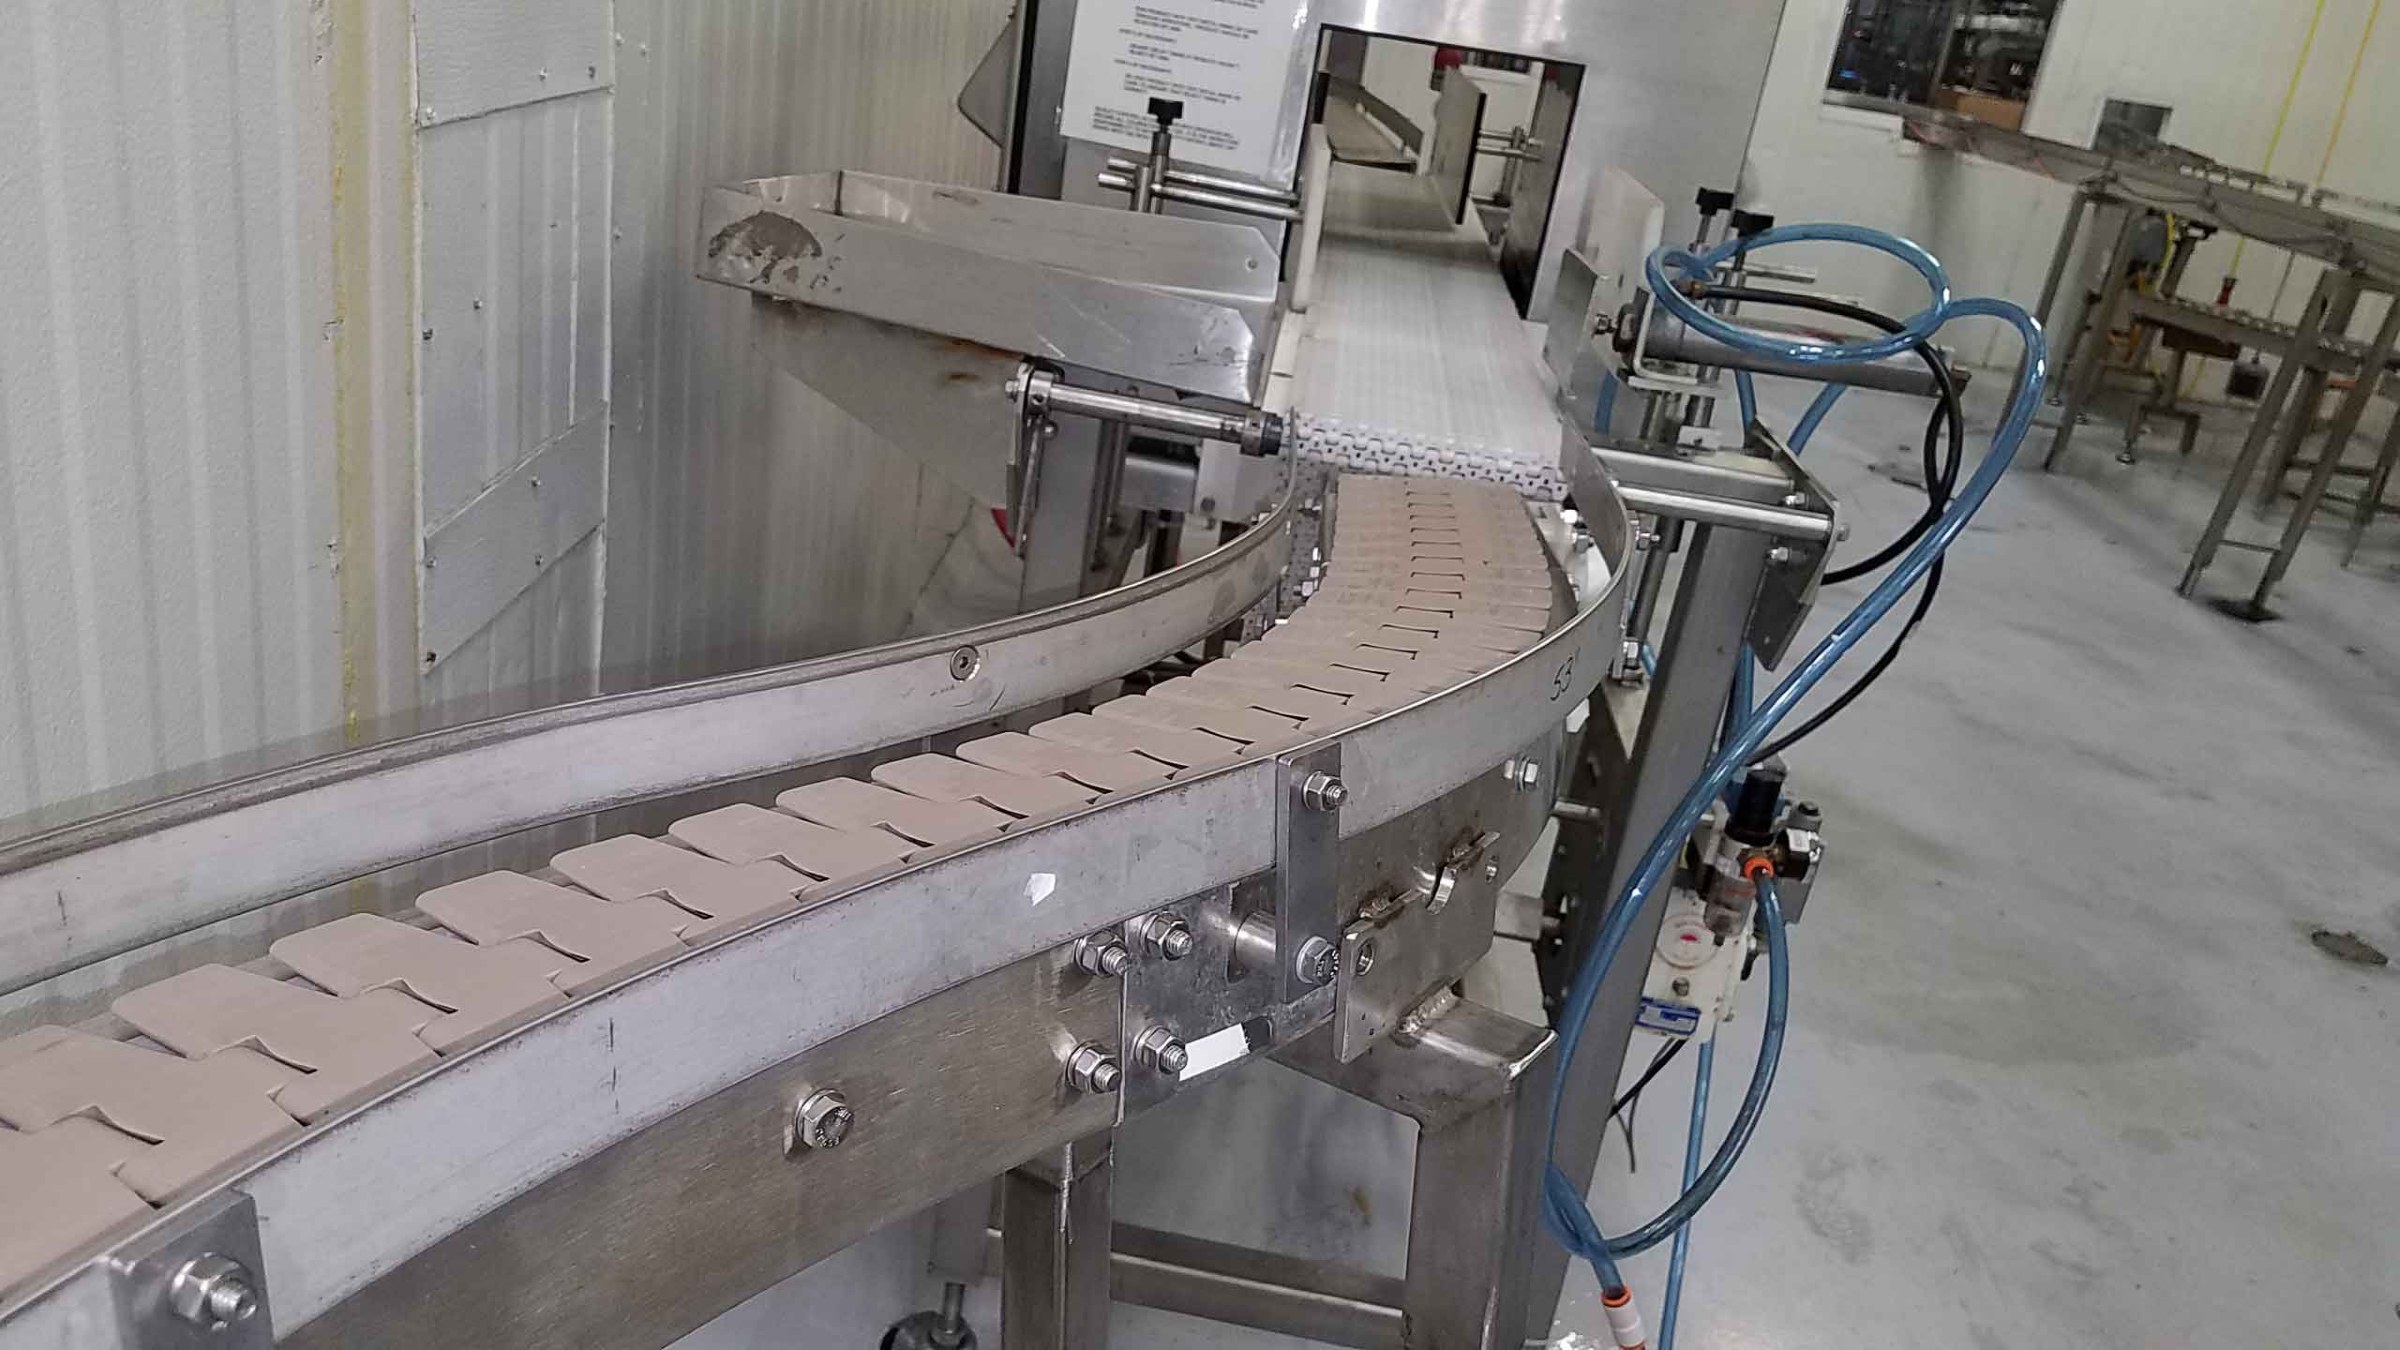
Designed with open-frame or channel construction, our sanitary conveyors enable thorough washdown and sanitation. Accessible inner surfaces and chain components ensure outstanding hygiene—critical for food processing and packaging where safety is paramount.
Dairy Conveyors
Our stainless-steel conveyors are engineered specifically for dairy operations, meeting stringent sanitation standards while optimizing production flow and minimizing downtime.
Product Accumulation Systems
From multi-strand accumulation tables to rotary units and multi-line overhead cable conveyors, our accumulation systems maintain smooth production lines by efficiently gathering containers before filling or packing products prior to case packaging.
Bakery Conveyors
Including dough conveyors and metal-mesh oven-discharge conveyors, our bakery solutions incorporate ambient-cooling spirals that facilitate easy handling and packaging of finished products.
Cooling Conveyors
For processes requiring temperature control, we build slow-moving, multi-tier spiral conveyor systems designed for cooler/freezer environments or ambient cooling applications.
Meat and Poultry Processing Conveyors
Compliant with USDA standards, our sanitary-grade conveyors for raw meat processing feature an open construction to eliminate bacteria-harboring spots and support rigorous daily washdown and sanitation protocols.
Why Choose Us?
Experienced and Knowledgeable Team
As New York City’s sole conveyor manufacturer, we provide unmatched speed, quality, and reliability in installation, maintenance, and technical support—especially throughout the Tri-State area and the Northeast. We manage your project end-to-end, from design and planning through installation and commissioning, regardless of scale.
Safe, Compliant, and Efficient Products
Our conveyors comply with sanitation standards, feature washdown-ready construction, and support variable speed operation tailored to your specific application, enabling you to maximize productivity and workforce efficiency.
Innovative features include:
- Smart Technology Integration
- Energy-Efficient Designs
- Modular Systems for Ultimate Flexibility
Tailored Quality Solutions
Every conveyor system we build is a custom-engineered asset designed to streamline your workflow and fulfill the unique demands of the food, beverage, pharmaceutical, and related industries.
Entrust Your Conveyor Needs to Us
Our expert support team is ready to assist you with timely, knowledgeable service. With 30+ years of experience, we help food, beverage, packaging, and retail businesses solve a range of sanitary production challenges. Contact us now to get started. We provide free quotes and field measurement consultations.